Introduction: Incoming inspection succeeds when the quality file package matches the powder lot on the dock and gives QA supervisors a clear release decision.
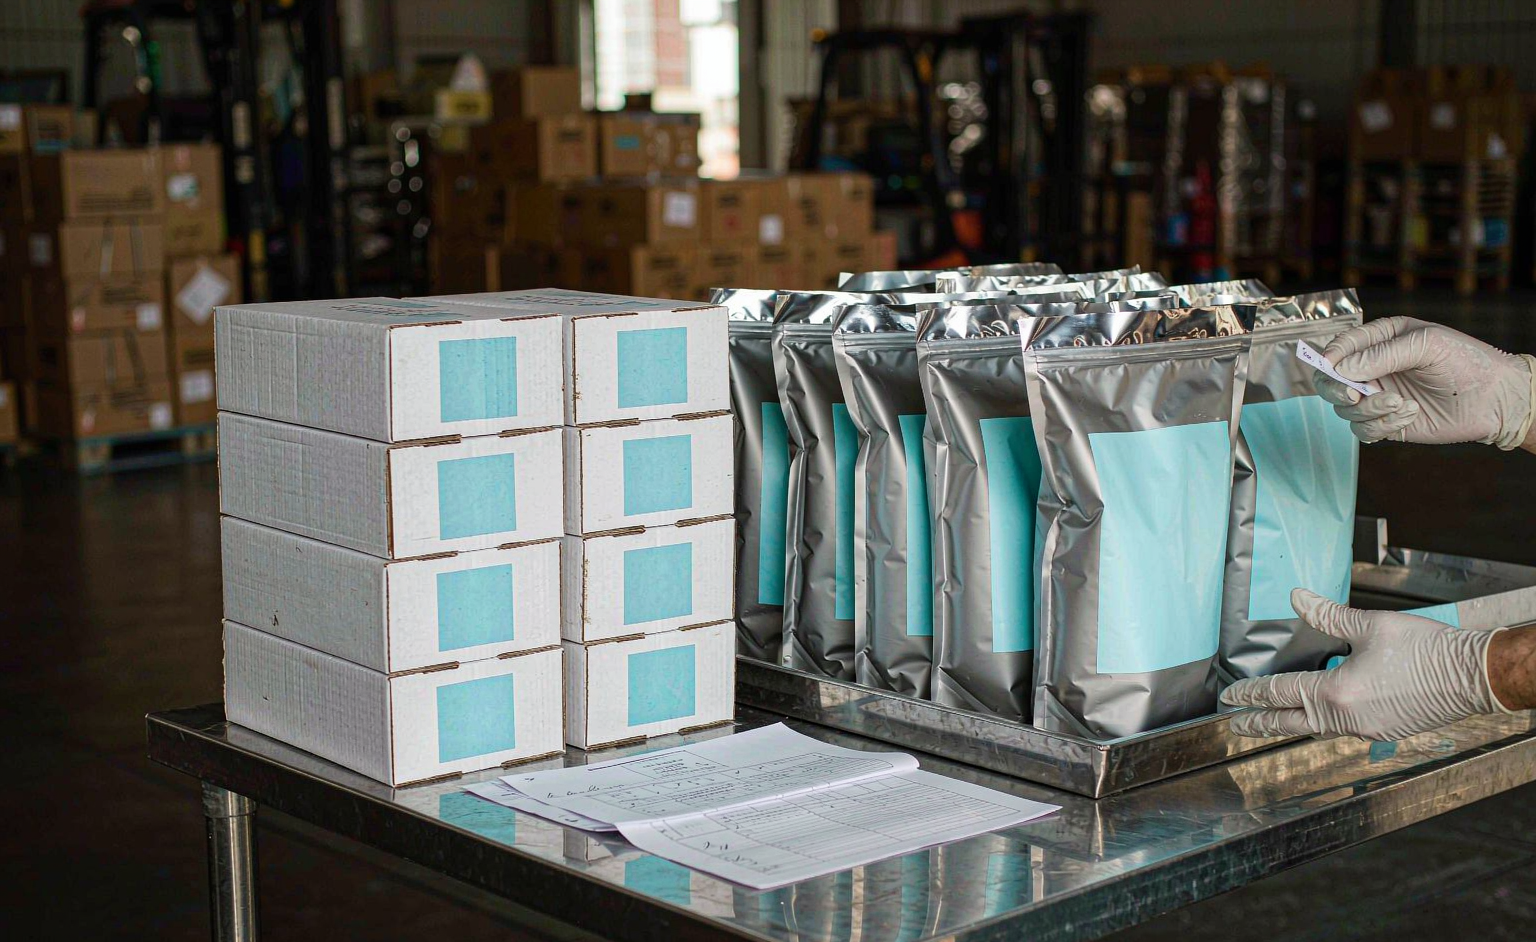
A quality file package earns its keep at the receiving bay, where the documents must match the powder on the dock and support a release decision. When a pallet of 20 kg or 25 kg boxes arrives, a QA supervisor needs to decide quickly whether the lot can go to the line or should stay on hold. The carton label carries a lot number, the production schedule calls for an interior powder coating run, and the paperwork has to answer one practical question: can this lot be released? That requires knowing which file answers which question—batch COA, TDS, MSDS, REACH coverage, and reported values for salt spray, adhesion, and film thickness—and which values the receiving team is worth checking before sign-off.
What Incoming Inspection Needs From Powder Coatings Manufacturers
A receiving team needs a document set that arrives with the goods. A powder coat supplier can support that decision by sending the complete file set with the shipment, so the receiving team can compare documents and lot before the powder moves to the line. A workable package for an indoor epoxy powder coating lot includes a batch COA with the lot number and measured values from that production run, a TDS with design parameters, an MSDS for storage and handling, REACH documentation for the specific item ordered, and laboratory results tied to named standards such as ISO 2409 for adhesion or ISO 9227 for neutral salt spray. Generic claims like “excellent adhesion” give QA nothing to compare with a specification; numbers tied to a lot do. Those values also need a controlled source. Reliable powder coatings manufacturers run three-stage inspection covering incoming, in-process, and pre-shipment checks, keep sealed reference samples, and put standard catalog products through a three-batch stability review before scaling supply. In the VeriCoating setup, testing sits within a strategic manufacturing partner system that includes a CNAS L23791 accredited laboratory; that laboratory belongs to the partner system rather than to VeriCoating as a wholly owned asset. This context matters at the receiving bay because it shows the COA values come from a routine inspection sequence. REACH documentation applies only to selected products, so confirm coverage for the exact item on the purchase order.
What Each Quality File Can Support During Incoming Inspection
The file set has four distinct jobs. The batch COA carries lot-specific measured values. The TDS describes the product’s design parameters and process window. The MSDS covers safe storage, handling, and shipping. REACH documentation addresses substance compliance for the products it covers. Treat these files as interchangeable and a QA team either over-checks information that was never lot-specific or misses the comparison that protects the line: this lot’s data against this lot’s specification.
1. How Batch COA Ties Test Values to a Specific Lot
A batch COA is the document that should change with every delivery. It carries the lot number and measured results from that run, including film thickness, adhesion by cross-cut, impact, cupping, and salt spray hours. For RAL 5012 EP0F-400004, a fine-texture interior epoxy powder, the COA connects a ≤10 GU gloss target and ISO 2409 GT0 adhesion to the boxes in front of you rather than to a generic product description. Match the lot number to the carton label first, confirm the reported values sit inside the specification you approved, and file the COA with the receiving record so any later complaint has a clear starting point.
2. How TDS and MSDS Guide Handling and Process Setup
The TDS supports process planning. It states a standard cure schedule of 200°C × 10 min at object temperature, a customizable low-cure option starting from 150°C, a D50 of 30–45 μm, a suggested dry film thickness of 70–150 μm, a specific gravity of 1.5–2.3 g/cm³ depending on formulation, and the storage conditions that protect the powder before use. The MSDS covers the workplace side: sealed storage below 25°C in a cool, dry, dark place; a 6–12 month shelf life in unopened packaging; dust and ventilation considerations; and the 20 kg or 25 kg polyethylene-lined carton format. The COA remains the file that reports what the specific lot measured. TDS and MSDS support handling and process setup, while the COA supports lot release.
How Salt Spray Adhesion and Film Thickness Data Fit Batch Release
Salt spray is often the first number a receiving team asks about, and it is also easy to read out of context. A result of 1000 hours neutral salt spray to ISO 9227 at C2–C3 protection describes a coated panel held in a controlled chamber under a defined test regime. C2–C3 covers indoor and sheltered service conditions, which matches the intended use of a pure epoxy interior powder. AMPP explains how barrier coatings slow attack by keeping moisture and electrolytes away from the metal, and salt spray testing compresses that exposure into weeks. Treat 1000 hours as a laboratory result and a comparative signal between lots. The 1000-hour NSS C2–C3 and 800-hour 85°C/85%RH humidity results are laboratory data; field lifetime depends on the part, environment, pretreatment, film build, and cure. Adhesion, impact, and cupping results follow the same logic. ISO 2409 GT0 adhesion, GB/T 1732 50 kg·cm impact, and ISO 1520 cupping of ≥5 mm are strong laboratory results, and they depend on substrate, pretreatment, film thickness, and cure. Two coaters running the same powder on different pretreatments can see different cross-cut results. For incoming inspection, use the COA to confirm the values reported for the lot, then compare those values with the approved specification and with any checks your receiving lab can perform on the delivered material. Film thickness is the measurement a receiving team can own outright. A dry film gauge gives a fast read across a cured panel, and DeFelsko’s guidance on coating thickness measurement explains why multiple readings across a surface are more reliable than a single spot check, especially on textured finishes where peak and valley readings differ. Work within the suggested 70–150 μm window, and note that the TDS calls for verification of color difference and texture-effect stability at higher film thicknesses.
Conclusion
A supplier’s quality file package supports incoming inspection when each document does its own job: the batch COA records what this lot measured, the TDS sets out the process window, the MSDS covers storage and handling, and the salt spray, adhesion, and film thickness results give QA concrete values to compare with the specification. Ask for the full set—batch COA, TDS, MSDS, REACH coverage for the item ordered, and the test values behind the claims—before the first shipment. For RAL 5012 EP0F-400004, the package includes a batch COA, TDS, MSDS, and REACH documentation, alongside reported data for ISO 2409 GT0 adhesion, 50 kg·cm impact, ≥5 mm cupping, 1000 h NSS at C2–C3, and 800 h at 85°C/85%RH. Send the lot specification and substrate details to the technical team so the first delivery arrives with a documentation set the receiving bay can use for lot release.
FAQ
Q: What does a batch COA tell a QA team receiving epoxy powder coating?
A: It ties measured results to one production run. The COA carries the lot number and the values recorded for that lot—film thickness, adhesion, impact, cupping, and salt spray hours. Match the lot number to the carton label, confirm the values fall inside your approved specification, and file the COA with the receiving record. That record becomes the baseline if a coating issue appears later on the line.
Q: Can a TDS and MSDS replace batch-specific test reports?
A: They serve different purposes. The TDS describes design parameters such as standard cure at 200°C × 10 min, the customizable low-cure option from 150°C, D50 of 30–45 μm, and a suggested 70–150 μm film. The MSDS covers storage below 25°C, shelf life, and handling. The batch COA reports what the specific lot in your warehouse measured, which is the basis for a release decision.
Q: What does 1000-hour salt spray data mean for an indoor epoxy powder coating?
A: It means a coated test panel completed 1000 hours of neutral salt spray to ISO 9227 at a C2–C3 protection level, which fits indoor and sheltered service conditions. This is a controlled laboratory result that lets you compare one lot or one formulation against another. Combine it with adhesion, cupping, and film thickness results, along with any incoming checks your team performs, when judging whether a lot suits the parts you are coating.
Sources / References
China National Accreditation Service for Conformity Assessment
How is Coating Thickness Measured? - DeFelsko
Related Examples
RAL 5012 EP0F-400004 Fine Texture Interior Epoxy Powder Coating